 Excavator
294 models
 Backhoe Loader
51 models
 Crane
68 models
 Concrete Mixer
79 models
 Wheel Loader
54 models
 Compactor / Roller
45 models
 Motor Grader
42 models
 Dozer
41 models
 Concrete Pump
66 models
 Skid Steer Loader
11 models
 Telehandler
13 models


Spray concrete at a rock face or a tunnel roof and, if the mix and the speed are right, it stays there without any mould. That sprayed material is shotcrete: mortar or concrete carried through a hose and shot at high speed onto a surface, where the force of the impact packs it tight.
India’s code for it is IS 9012, the Bureau of Indian Standards’ recommended practice for shotcreting. It covers the dry-mix and wet-mix processes, and most figures below come from it. Site crews often call the work guniting. The pumping side of a sprayed-concrete job belongs with concrete pumps and the transit mixers that feed them, covered near the end.
What is shotcrete, and what else is it called?
Shotcrete is concrete or mortar placed by spraying instead of pouring. IS 9012 defines it as mortar or concrete “conveyed through a hose and pneumatically projected at high velocity on to a surface”, and adds that the force of the jet is what compacts it. Pneumatic simply means driven by compressed air.
Because the jet does the compacting, there is no vibrator and usually no formwork. The mix is kept stiff, so it holds on a wall or overhead without sagging.
The standard lists its other names (gunite, sprayed concrete, spraycrete, air-blown mortar, gunned concrete) and settles on shotcrete as the internationally accepted word. On Indian sites and in tenders you will also meet guniting for the work and gunite for the dry-mix material.
How does the shotcrete process work?
Every job has a mix, a machine that pushes it into a hose, compressed air, and a nozzle held by a trained operator called the nozzleman. The two processes differ in where the water joins the mix.
In the dry-mix process, cement and moist sand are mixed first and fed into a machine the standard calls the delivery equipment, or gun. A feed wheel pushes the mix into the hose. Compressed air carries it along, and water is added only at the nozzle, through a ring of small holes inside it. The nozzleman sets the water by hand, second by second.
In the wet-mix process, every ingredient, water included, is mixed before it reaches the machine. The finished concrete is pushed down the hose, by air or by a pump, and extra air is blown in at the nozzle to speed it up and shape the spray.
Where the water joins the mix in each process
In dry mix the water meets the cement at the nozzle, so the mix is finished on the wall itself. In wet mix it was finished earlier, at a batching plant or in a transit mixer, where it could be weighed.
Dry mix vs wet mix shotcrete: which one should you use?
Neither wins everywhere. IS 9012 says either process can give shotcrete good enough for normal construction, and that the cost of the equipment, its upkeep and the way the job runs usually decide. The working differences look like this.
| Point | Dry mix | Wet mix |
|---|---|---|
| Where the water goes in | At the nozzle, controlled by the nozzleman | At the mixer, before the hose |
| Changing the water | Instant, at the nozzle | Fixed once the batch is mixed |
| Rebound and dust | Higher | Lower |
| Stopping and restarting | Easy; the dry material clears out of the hose | Needs care; wet concrete left in the hose can set and block it |
| Volume placed | Smaller | Larger, in less time |
| Usual fit | Repairs, small jobs, work with frequent stops | Tunnel lining, large slopes, long continuous runs |
The dry process asks more of the nozzleman, because water and dry mix are not fully combined until they strike the surface. Its strength is control: the water changes instantly, and the hose stops and starts without fuss.
Wet mix trades that control for output and less dust. Its weak point is the hose: concrete left standing in a line stiffens, and how a blocked line is cleared safely is set out in our guide to concrete pump line blockage.
Shotcrete vs gunite: are they the same thing?
Mostly, with one catch. Gunite began as a trade name. The American taxidermist Carl Akeley first used a “cement gun” in 1907 to repair a crumbling museum front in Chicago, blowing dry material through a hose and adding water at the nozzle, and in 1911 he was granted a patent covering both the gun and the gunite it produced. Gunite is therefore, strictly, the dry-mix method. IS 9012 says exactly that: gunite, marked as a trade name, is a “method of applying dry-mix shotcrete”.
Shotcrete is the umbrella word for both processes, and that is how the Indian standard uses it from start to finish. The one trade that keeps the words apart is swimming pool building, where shotcrete means wet mix and gunite means dry mix. On an Indian tender, do not rely on the word guniting to tell you which process is wanted. Read which process the specification names.
What is the mix for shotcrete?
The ingredients are ordinary concrete materials, held to tighter limits because everything passes through a hose.
| Ingredient | What the standard asks |
|---|---|
| Cement | Ordinary, rapid-hardening, Portland slag, Portland pozzolana, high-strength ordinary or hydrophobic Portland cement, with the engineer’s approval |
| Sand | To IS 383, graded evenly from fine to coarse, Zone II or Zone I to II |
| Coarse aggregate (stone) | Nominal maximum size of 10 mm, 12.5 mm or 20 mm; oversize pieces screened out because they plug the hose |
| Water-cement ratio | Usually 0.35 to 0.50 by mass in place, lower than most ordinary concrete |
| Admixtures | Only when specified, and then meeting IS 9103 |
| Steel | Bars normally no thicker than 16 mm, or welded wire mesh no tighter than 50 x 50 mm, so the spray can get behind it |
Sand grading matters: finer sand shrinks more as it dries, coarser sand bounces off more. Which bagged cement suits which job is covered in our guide to choosing cement by type and grade, and the stone sizes a crusher produces are explained in aggregate sizes from 6 mm to 40 mm.
Trial mixes come before the real work. For dry mix, IS 9012 suggests trying cement to sand between 1:3 and 1:4.5. For wet mix with stone in it, start at 20 to 40 percent coarse aggregate and adjust from the first result. Dry-mix sand should carry 3 to 6 percent moisture so it flows down the hose evenly, without slugs. An accelerator, the admixture that speeds up setting, is used only where the specification calls for it; how the admixture types differ is set out in our guide to concrete admixtures and IS 9103.
What is rebound in shotcrete, and how much is normal?
Rebound is the sand, stone and cement paste that bounces off the surface instead of sticking. Some of it cannot be avoided. How much you lose depends mostly on which way the nozzle is pointing.
| Surface being sprayed | Rebound, percent |
|---|---|
| Floors and slabs | 5 to 15 |
| Sloping and vertical walls | 15 to 30 |
| Overhead work | 25 to 50 |
Nozzle angle, air pressure, water and cement content, aggregate grading, the amount of steel and layer thickness all move it. It is heaviest in the first seconds and drops once a soft cushion of fresh shotcrete builds up.
Rebound is leaner and coarser than the mix that went in, so what stays on the wall carries more cement: slightly stronger, but more inclined to crack as it shrinks. And IS 9012 says rebound must never be worked back into the job or saved for a later batch, because it can be contaminated and has lost part of its cement. Sweep it away.
Plan the material order around it. On an overhead job up to half of what leaves the nozzle can end up on the floor. Work out the cement, sand and stone for the finished volume with the method in our guide to calculating cement, sand, aggregate and steel, then add an allowance for the rebound range in the table.
How is shotcrete applied on site?
Most failures start before the nozzle opens: on repairs, IS 9012 blames poor surface preparation more than any other single factor. The order of work runs like this.
- Prepare the surface. Earth, as in a canal lining, is compacted and trimmed to line and level. Old concrete is chipped back to sound material, with tapered edges and no square shoulders. Never shoot onto a frozen or spongy surface, or one with free water on it, and keep the surface damp for several hours beforehand.
- Fix the steel and the guides. Wire bars firmly so the spray cannot shake them, and stretch ground wires to mark the finished thickness.
- Shoot in loops. The nozzle is held 0.5 to 1.5 m (about 1.6 to 4.9 feet) from the surface, square to it, and moved in small circles from side to side and up and down. When covering bars it goes closer and at a slight angle, so the shotcrete packs in behind them.
- Build walls from the bottom up. On a thick layer, keep the top at roughly 45 degrees so rebound falls clear of the work.
- Layer and joint with care. Let each layer take its initial set, broom off loose material, and tap the surface with a hammer for hollow, drummy spots, which are cut out and refilled. Joints are tapered to a thin edge over about 300 mm (1 foot).
- Stop in high wind or rain, and end each day’s work on a thin, sloped edge.
- Cure. Keep the surface continuously wet for at least 7 days. Shotcrete sections are thin and rough, so they dry out faster than a poured slab.
Leave the natural nozzle finish; trowelling it smooth can disturb the bond. The ways of keeping fresh concrete wet, and when a sprayed membrane is used instead, are covered in our guide to curing compound for concrete.
How strong is shotcrete?
Done well, about as strong as ordinary concrete or mortar of the same mix. IS 9012 puts most reported 28-day strengths between 20 and 50 N/mm² (MPa), and advises asking for more than 25 N/mm² only on the most carefully run jobs. Drying shrinkage is usually 0.06 to 0.10 percent. That is higher than most stiff poured concrete, so expect more shrinkage cracks and plan joints closer together.
The bigger variable is the crew; the standard compares shotcrete to welding. So testing starts before the job. The same crew, machine and mix shoot test panels at least 75 x 75 cm and 7.5 cm thick, one for each position on the structure (slab, wall, overhead), and cores or cubes from them are crushed at 7 or 28 days. Every cut face must be dense, with no layers and no sand pockets.
During the work, smaller panels (at least 30 cm square, 75 mm thick) or 15 cm cube moulds gunned directly are tested, and cores from the structure plus hammer-sounding of each layer close the loop.
Where is shotcrete used in India?
Wherever a surface is hard to box in with formwork.
- Tunnel linings for roads, railways and metros, and roadways in underground mines, where it keeps loose rock from falling.
- Rock and soil slopes along hill roads and rail cuttings, often sprayed over steel mesh.
- Canal linings, sprayed onto trimmed and compacted earth.
- Repairs to spalled or damaged concrete on bridges, tanks and buildings, where the dry process is common.
- Temporary support for deep basement digs, and swimming pool shells.
For tunnel work, current bridge and tunnel projects, and the machines a contractor can put to work on them, are gathered on our bridge and tunnel construction equipment page. Underground mining, where sprayed support comes in, is explained in our guide to types of mines in India.
What machines are needed for shotcrete?
A dry-mix rig needs a mixer, a gun, an air compressor and a water supply. IS 9012 asks for at least 1 minute of mixing in a drum mixer, and it refers the gun itself to IS 6433, the Indian specification for guniting equipment. The compressor needs a moisture separator and enough capacity to keep the nozzle speed up while also running a blow pipe that clears away rebound. At the gun, air pressure should be at least 0.3 N/mm² (3 bar) for hose up to 30 m long, plus 0.035 N/mm² (0.35 bar) for every extra 15 m of hose and for every 7.5 m the nozzle sits above the gun. Water at the nozzle must be at a higher pressure than the air, with a booster pump if the line pressure falls short.
A wet-mix rig needs mixed concrete from a batching plant or ready-mix truck, a machine to push it down the hose, and a compressor feeding an air ring at the nozzle. On large tunnel jobs the nozzle is mounted on a mechanical arm and worked by remote control.
Stationary concrete pumps such as the Schwing Stetter SP 1600 (theoretical output up to 64 m³ an hour, as listed in October 2026) and the Schwing Stetter SP 2000 (up to 73 m³ an hour) are built to move large volumes of concrete into formwork. A spraying system has one extra demand: the flow must be as steady as possible, because every pulse in the hose shows up as an uneven spray. Before feeding a nozzle from any concrete pump, ask the dealer whether it runs at a low, steady output and takes a spraying nozzle and air ring. How a pump’s output and pressure figures are rated, and what they mean on site, is explained in our guide to concrete pump output and pressure. Dedicated shotcrete machines and robotic spraying arms are specialist tunnelling plant not sold through DesiMachines; confirm those with the maker.
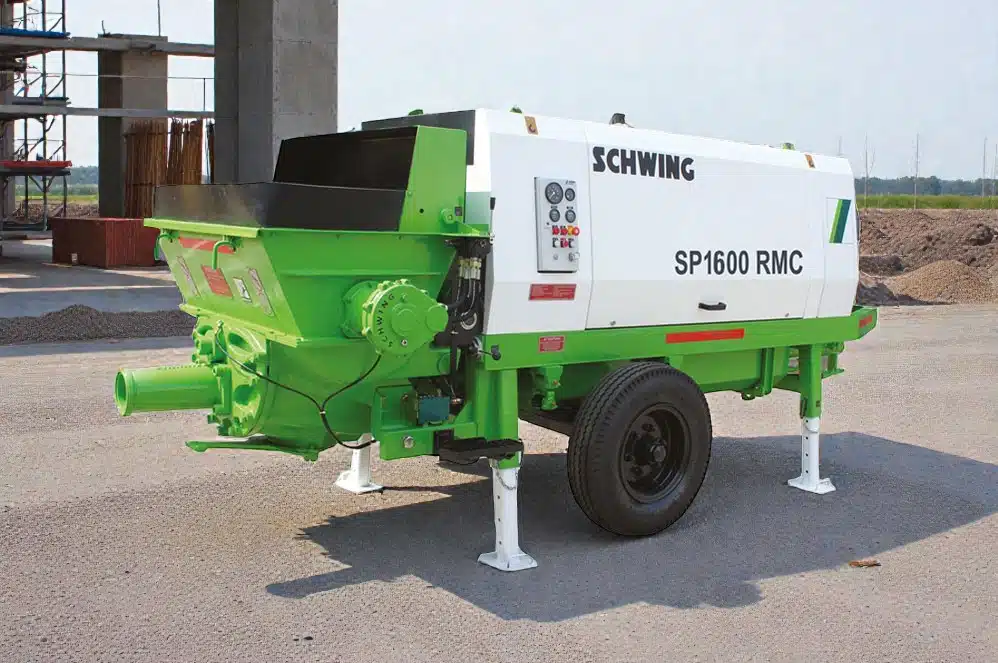
If your sprayed-concrete job needs a pump, compare stationary concrete pump models and prices and tell the dealer the output and hose length you need.
How do you plan a shotcrete job?
Start with the surface, not the machine. Pick the process from the job, fix the mix by trial panels, add the rebound allowance to the material order, and have the nozzleman shoot test panels first.
Where shotcrete sits beside cement, aggregate, admixtures and curing is mapped in our building materials guide. For the concrete that feeds a wet-mix rig, compare transit mixer and concrete mixer models, and for the pump, concrete pump models and prices. The practice described above follows IS 9012:1978, Recommended practice for shotcreting, with the history of gunite drawn from the Wikipedia article on shotcrete.
Prices, specifications and features are indicative, vary by variant, location and date, and should always be confirmed with the official OEM or authorised dealer before any purchase decision. DesiMachines is not liable for decisions taken on the basis of information that may have changed after publication.
Machines, tenders and news for this industry: Building Construction