 Excavator
294 models
 Backhoe Loader
51 models
 Crane
68 models
 Concrete Mixer
79 models
 Wheel Loader
54 models
 Compactor / Roller
45 models
 Motor Grader
42 models
 Dozer
41 models
 Concrete Pump
66 models
 Skid Steer Loader
11 models
 Telehandler
13 models


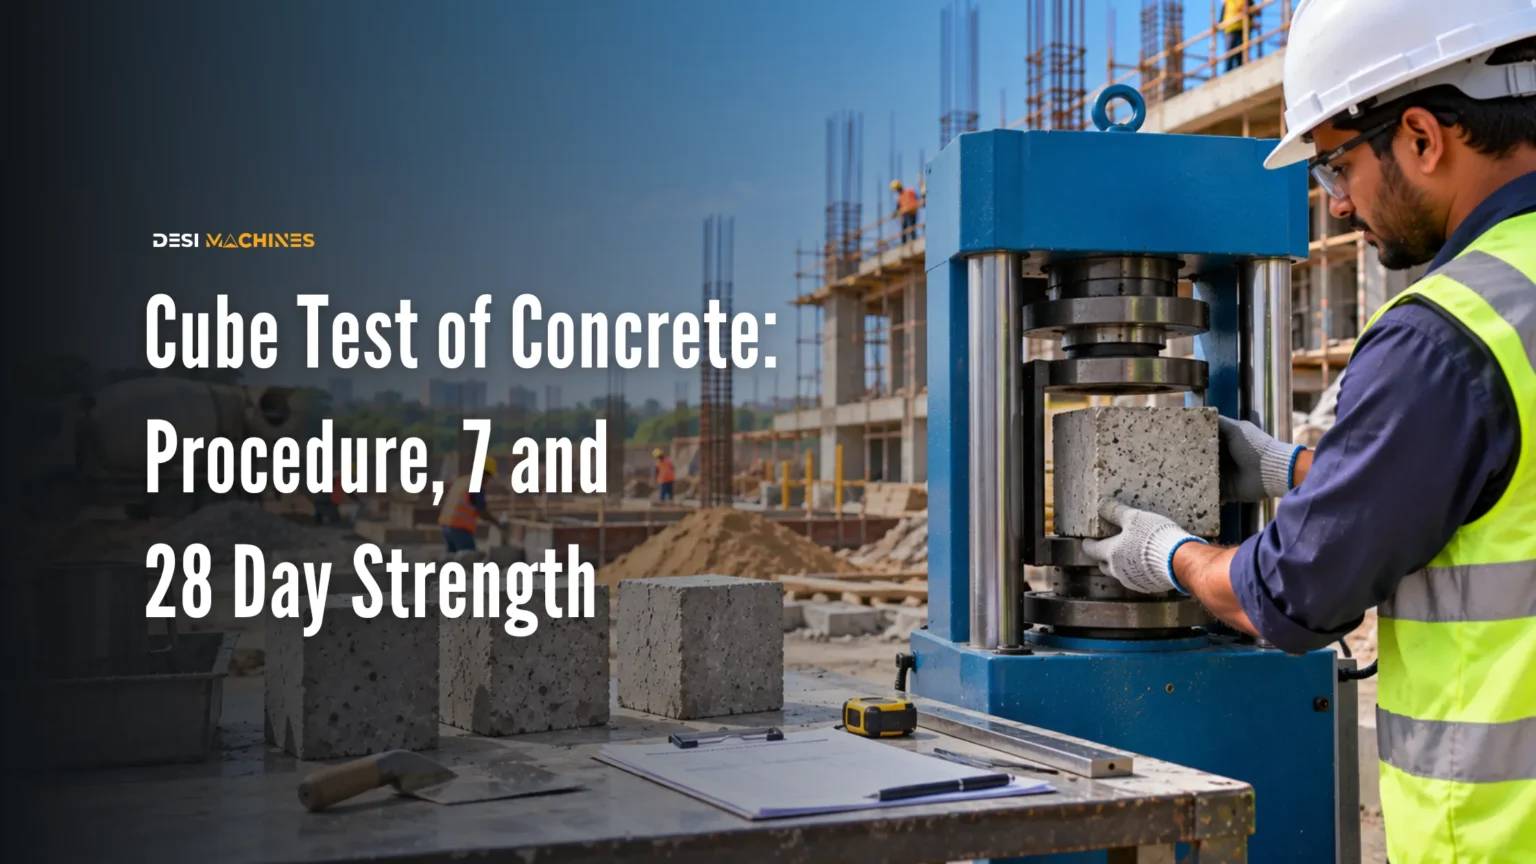
Three 150 mm concrete cubes, cast from the same batch that went into your slab and crushed in a testing machine 28 days later, are how an Indian site proves its concrete is as strong as ordered. Each cube’s breaking load in newtons, divided by its 22,500 mm² face, gives its compressive strength in N/mm², and the average of the three is the result for that sample.
The slump test tells you, on the day, whether concrete can be placed. The cube test tells you, a month later, whether it will carry the load. This guide covers the mould and the tools, how to cast and cure the cubes, how the lab breaks them, what 7-day and 28-day results mean, how many cubes the code asks for, how to read a set of results against IS 456, and what happens when cubes fail.
What is the cube test of concrete?
It is a compression test on small cubes of the concrete you are using. The cubes are cast on site, kept wet, and then squeezed between the steel plates of a compression testing machine until they break. The highest load the cube carried gives its compressive strength, which is the property engineers design concrete around.
The strength is written in N/mm² (newtons per square millimetre). One N/mm² is the same as one MPa, so 20 N/mm² and 20 MPa mean the same thing. The grade name carries this number: IS 4926, the ready-mixed concrete code, defines the grade as the characteristic compressive strength of a 150 mm cube at 28 days, written as “M” followed by that value. So M20 is concrete whose 28-day cube strength is 20 N/mm².
“Characteristic” has a precise meaning here. IS 456:2000, the main Indian code for plain and reinforced concrete, defines it as the strength below which not more than 5 percent of test results are expected to fall. That is why a mix is designed to average well above its grade and why the acceptance rules further down look at groups of results, not one cube.
Three standards share the job. IS 1199 (Part 5):2018 covers making and curing the cubes. IS 516 (Part 1/Section 1):2021 covers breaking them, in place of the matching part of the old IS 516:1959. IS 456 clauses 15 and 16 say how many to make and when the concrete passes.
Cube mould size and the tools you need
The standard cube is 150 mm on every side (about 6 inches). A 100 mm cube is allowed only when the largest stone in the mix is 20 mm or smaller. Moulds are made to IS 10086, and each one carries an identification number, welded, painted or tagged on.
Table 1: Cube test equipment as per IS 1199 (Part 5):2018 and IS 516 (Part 1/Sec 1):2021
| Item | What the standard asks for |
|---|---|
| Cube mould | 150 mm × 150 mm × 150 mm; 100 mm cube allowed if the largest aggregate is 20 mm or less; tolerances as per IS 10086 |
| Tamping rod | Round steel, 16 ± 1 mm diameter, 600 ± 5 mm long, rounded ends |
| Tamping bar (alternative) | Square steel ramming face of 25 mm, at least 400 mm long, about 2 kg, with a handle |
| Vibrator (alternative) | Needle (immersion) vibrator of at least 120 Hz, or a vibrating table of at least 40 Hz |
| Small tools | Scoop about 100 mm wide, steel trowel or float, mallet, mould oil, sampling tray at least 900 mm × 900 mm × 50 mm deep |
| Testing machine | Compression testing machine to IS 14858, calibrated at least once a year and in calibration on the day of the test |
Before every use, check that the mould bolts tighten fully and that the base plate sits flat. A thin coat of mould oil goes on the inside faces, on the joints between the mould sections, and between the mould and its base plate, so that cement water does not leak out while you fill it.
How to cast concrete cubes on site, step by step
Take the sample from the batch going into the work, the way IS 1199 (Part 1) describes, and turn it over on the tray with a shovel before you start. Then:
- Set the oiled mould on a firm, level surface where nothing is vibrating.
- Fill it with a scoop in layers of roughly equal depth, none thicker than 50 mm. For a 150 mm cube that means three layers. Move the scoop round the top edge as the concrete slides off, so it spreads evenly.
- Compact each layer as soon as it is in. With the 16 mm rod, give a 150 mm cube at least 35 strokes per layer, and a 100 mm cube at least 25, spread evenly over the area. Do not let the rod hit the bottom of the mould on the first layer, or go far into the layer below on the next ones.
- After rodding each layer, tap the sides of the mould with the mallet until large air bubbles stop coming up and the rod holes close.
- Put just enough concrete in the last layer to fill the mould. Adding a little and compacting it again is fine; scraping off a big heap is not.
- Level the top with a trowel, cover it so it does not dry out, and mark the cube clearly. Write down the date and time, the grade, the slump, where the batch went and how you compacted it.
The method of compaction follows the slump. For concrete below 50 mm slump, IS 1199 (Part 5) prefers a vibrating table or a needle vibrator. Between 50 and 100 mm, any of the methods will do. Above 100 mm, use the rod or the bar. If you vibrate, stop as soon as the surface turns smooth and glassy; more vibration only pushes the stones down and brings water up. The slump test of concrete guide explains how to measure that slump first.
A cube that is badly made tells you about the person who made it, not about the concrete. IS 516 says a badly honeycombed cube is not representative of the concrete supplied and should not be tested; if one is tested, the report has to say so.
How are concrete cubes cured before testing?
Curing here means keeping the cube wet and at a steady temperature so the cement keeps reacting. IS 1199 (Part 5):2018 sets a simple routine:
- Leave the cube in its mould for at least 16 hours and not more than three days, counted from the time water was added to the mix. Keep it at 27 ± 3 °C, away from shock and vibration, with the top covered.
- After demoulding, put it straight into clean water at 27 ± 2 °C, or into a moist room at 27 ± 2 °C and at least 95 percent humidity, until just before the test.
- If the cubes go to an outside laboratory, wrap them in wet cloth, wet sand or sawdust, or seal them in plastic bags with water, and deliver them damp at least 24 hours before the test. The lab then keeps them in water at 27 ± 2 °C.
Most cube failures that turn out to be false alarms start here. A cube left on the site office roof in May, or carried to the lab dry in the back of a pickup, has not been cured the way the code assumes. The structure might be fine and the cube still read low. Curing of the slab itself is a separate job; how long it needs is covered in the post on the curing period for a slab.
Cube test procedure and formula
On test day the laboratory follows IS 516 (Part 1/Section 1):2021, clause 3:
- Take the cube out of the water no more than 2 hours before testing and keep it under a wet cloth until then. Wipe off surface water.
- Measure the cube to the nearest 0.2 mm and weigh it.
- Clean the machine’s plates. Use no packing between the cube and the plates.
- Place the cube so the load presses on two of its side faces, at right angles to the direction it was filled. The rough trowelled top never faces a plate. Centre it to within 1 percent of its size.
- Apply load smoothly, without shock, at a steady 14 N/mm² per minute until the cube can take no more. Record the maximum load.
- Look at how it broke and record whether the failure was satisfactory.
For a 150 mm cube, 14 N/mm² per minute works out to 315 kN per minute (about 32 tonnes of force each minute). A cube near 26 N/mm² therefore breaks a little under two minutes after loading starts. Loading much faster than this tends to give a higher reading than the concrete deserves.
A good break cracks all four exposed sides about equally, leaving a shape like two pyramids meeting at their tips. IS 516 Figure 2 draws nine bad breaks, among them a sideways crack across one face, one side sheared off at a slant, and a corner breaking away. The lab records which one the cube looked like, and an unsatisfactory break is a reason to look hard at that result.
The strength is the load divided by the loaded area:
Compressive strength (N/mm²) = maximum load (N) ÷ loaded area (mm²)
The area of a 150 mm cube is 150 × 150 = 22,500 mm². The result is stated to the nearest 0.5 N/mm². The average of the three cubes is the result for that sample, provided no single cube is more than 15 percent above or below the average.
Table 2: Worked example, one sample of three 150 mm cubes at 28 days
| Cube | Maximum load | Strength (load ÷ 22,500 mm²) |
|---|---|---|
| A | 545 kN (545,000 N) | 24.2 N/mm² |
| B | 590 kN (590,000 N) | 26.2 N/mm² |
| C | 615 kN (615,000 N) | 27.3 N/mm² |
| Average | – | 25.9 N/mm², reported as 26.0 N/mm² |
| 15 percent check | – | Allowed band 22.0 to 29.8 N/mm²; all three cubes inside, so the sample is valid |
Now suppose cube A had broken at 400 kN, which is 17.8 N/mm². The average drops to 23.8 N/mm², and 17.8 sits more than 15 percent below it. IS 456 clause 15.4 calls that sample invalid. IS 516 (2021) says to repeat the test, and if no spare cube is left, to take the average of the two closest values instead: 26.2 and 27.3 average 26.8, reported as 27.0 N/mm². That is one reason to cast a spare cube or two.
What is 7-day and 28-day strength of concrete?
They are the cube results at 7 days and at 28 days after water was added to the mix. IS 516 names 7 and 28 days as the usual test ages. It also allows 24 hours and 72 hours for early strength, and recommends 56 days, 90 days and one year when a later strength is wanted.
The 28-day result is the only one that decides whether concrete is accepted. IS 456 clause 15.1.1 is plain about it: 7-day compressive tests are optional, they give a quicker idea of the quality, and “the 28 days compressive strength … shall alone be the criterion for acceptance or rejection of the concrete”. IS 4926 repeats the same sentence for ready-mixed concrete.
So what should a 7-day cube read? IS 456 gives no fixed percentage. It says the 7-day value should be arrived at from actual testing. The share of strength concrete has gained by day seven depends on the cement, the water-cement ratio, admixtures and temperature, so the useful 7-day figure is the one your own mix has shown in trial cubes. Once you have that, a 7-day set far below the usual pattern is an early warning: check the batch records and curing straight away, three weeks before the 28-day cubes confirm or clear it.
Some sites also cast extra cubes to decide when formwork can come off. IS 456 clause 15.3 allows additional cubes for exactly this, and for checking how long to cure.
How many cubes per cubic metre of concrete?
IS 456 clause 15.2.2 sets a minimum number of samples by the quantity of each grade placed. Every sample is three cubes for the 28-day test (clause 15.3). Cubes for 7 days or for formwork stripping are extra.
Table 3: Minimum sampling frequency as per IS 456:2000, clause 15.2.2
| Quantity of concrete in the work | Number of samples | Cubes for the 28-day test |
|---|---|---|
| 1 to 5 m³ | 1 | 3 |
| 6 to 15 m³ | 2 | 6 |
| 16 to 30 m³ | 3 | 9 |
| 31 to 50 m³ | 4 | 12 |
| 51 m³ and above | 4, plus 1 for each further 50 m³ or part of it | 12, plus 3 for each further 50 m³ or part of it |
Two notes in the clause matter on site. At least one sample has to be taken from each shift. And sampling should be random and spread over the whole pour and every mixer, so that each batch has a fair chance of being tested.
Worked example: a 120 m³ slab in M25. The first 50 m³ needs 4 samples. The remaining 70 m³ is one full 50 m³ plus part of another, so 2 more. That is 6 samples, or 18 cubes for 28 days. If you want 7-day results too, add three cubes per sample.
For ready-mixed concrete, IS 456 lets the supplier and buyer agree the frequency. IS 4926 clause 6.3.2 sets the producer’s own minimum at one sample for every 50 m³ or every 50 batches, whichever gives more samples. The buyer can test separately, and on a structural pour should. The RMC vs site mix guide covers what else to agree with a supplier.
Acceptance criteria of cube test as per IS 456
IS 456 clause 16.1 accepts the concrete when two conditions are met together. The mean of any group of four non-overlapping consecutive results must meet the first limit, and every individual result must meet the second. Here a “result” means one sample, that is, the average of its three cubes.
The table as first printed in 2000 had separate rows for M15 and for M20 and above, with an individual limit of the grade minus 3 N/mm² for M15 and minus 4 N/mm² for M20 and above. Later amendments merged them. As amended, Table 11 reads, for M15 and above:
- Mean of 4 results: at least the grade (fck) plus 0.825 times the established standard deviation, rounded to the nearest 0.5 N/mm², or fck plus 3 N/mm², whichever is greater.
- Each individual result: at least fck minus 3 N/mm².
- Small pours: up to 30 m³, where fewer than four samples are taken, the mean of all samples must reach fck plus 4 N/mm² and each result at least fck minus 2 N/mm². With only one sample, it must reach fck plus 4 N/mm².
Standard deviation measures how far your results scatter from batch to batch. Until a site has 30 results of its own, IS 456 Table 8 gives values to assume: 3.5 N/mm² for M10 and M15, 4.0 for M20 and M25, and 5.0 for M30 to M50. Plugging those in gives the figures most sites work to.
Table 4: Pass marks using the assumed standard deviation (IS 456 Table 11 as amended, with Table 8)
| Grade | Assumed standard deviation | Mean of 4 results, at least | Each result, at least | Pour up to 30 m³: mean / each, at least |
|---|---|---|---|---|
| M20 | 4.0 N/mm² | 23.5 N/mm² | 17 N/mm² | 24 / 18 N/mm² |
| M25 | 4.0 N/mm² | 28.5 N/mm² | 22 N/mm² | 29 / 23 N/mm² |
| M30 | 5.0 N/mm² | 34.0 N/mm² | 27 N/mm² | 34 / 28 N/mm² |
| M35 | 5.0 N/mm² | 39.0 N/mm² | 32 N/mm² | 39 / 33 N/mm² |
For M20 the arithmetic is: 0.825 × 4.0 = 3.3, rounded to 3.5, so 20 + 3.5 = 23.5 N/mm². That beats 20 + 3 = 23, so 23.5 is the mark.
The figure below puts the M20 numbers on one line. The mix designer aims well above the pass mark on purpose: IS 10262:2019 sets the target mean at the grade plus 1.65 times the standard deviation, or the grade plus a fixed margin if that is higher. For M20 that gives 26.6 N/mm², so that ordinary batch-to-batch scatter still leaves the group mean above 23.5.
Figure 1: The M20 numbers, from the lowest single result allowed to the mix design target
All values in N/mm² at 28 days, using the assumed standard deviation of 4.0 N/mm². Bar lengths are drawn to scale against 30 N/mm². The design target and how the water-cement ratio is chosen to reach it are covered in the guide to the water cement ratio.
How to read a real set: four consecutive M25 results of 29.5, 31.0, 27.5 and 30.0 N/mm² average 29.5, above 28.5, and the lowest, 27.5, is above 22. That group passes. If one result had been 21.5, the group mean might still pass, but that one batch fails the individual limit. IS 456 clause 16.3 says only the batch that sample came from is then at risk, while a failed group mean puts all the batches between the first and last sample of the group at risk, capped at 60 m³ when no sampling rate was agreed. Each grade is judged separately.
What happens if the cube test fails?
Check the test before you doubt the slab. Look for these first:
- Were the three cubes of a sample within 15 percent of each other? If not, the sample is invalid, not failed.
- Does the lab report show satisfactory failure patterns, a calibrated machine and the right loading rate?
- Were the cubes honeycombed, demoulded too early, left dry, or carried to the lab without being kept damp?
- Do the batch records, slump readings and delivery tickets for that batch show anything unusual, such as extra water added at site?
If the cubes were made and tested properly and still fail, IS 456 clause 16.4 says the structural adequacy of the affected parts has to be investigated. The usual next step is a core test under clause 17.4. Cylinders are drilled out of the actual member and crushed, which tests the concrete in place, after its real compaction and curing.
- The engineer-in-charge picks the locations. At least three cores are tested.
- IS 516 (Part 4):2018 asks for cores of 100 to 150 mm diameter, with 100 mm preferred when the largest stone is 20 mm or less, and a length about twice the diameter. Lengths from one to two times the diameter are allowed with a correction.
- The core’s strength is corrected for its length using F = 0.11 × (length ÷ diameter) + 0.78, then multiplied by 5/4 to turn the cylinder value into an equivalent cube strength.
- The concrete is acceptable if the average equivalent cube strength of the cores is at least 85 percent of the grade’s cube strength for that age, and no single core is below 75 percent.
For M20 at 28 days that means an average of at least 17 N/mm² and no core below 15 N/mm². A 100 mm core 150 mm long (length ÷ diameter = 1.5) that breaks at 19 N/mm² gets a factor of 0.11 × 1.5 + 0.78 = 0.945, giving 18.0 N/mm² as a cylinder, or 22.4 N/mm² as an equivalent cube. That core passes.
If the cores also fall short, clause 17.6 allows a load test on the member. Anything beyond that, from strengthening to breaking out and recasting, is a decision for the structural engineer. A core hole also has to be filled properly afterwards, and how cavities in hardened concrete are repaired is covered in the guide to honeycombing in concrete.
How to keep cube results on the right side
Most of the gap between a pass and a fail is decided before the cube is made. The Table 8 values assume good site control: proper cement storage, weigh batching of all materials, controlled water, regular checks of aggregate grading and moisture, and regular workability and strength tests. Where that control is missing, the note to Table 8 adds 1 N/mm² to the assumed standard deviation. For M20 that pushes the assumed value from 4.0 to 5.0, and the mean pass mark from 23.5 to 24.0 N/mm², so the whole mix has to be richer to pass reliably.
Weighing materials is the single biggest step a small site can take. A self-loading concrete mixer with an on-board weighing system batches by weight in the field. The AJAX ARGO 4800 and the JOHN SLCM 4.3 list load-cell weighing, and the CONMAT CSLM 4300 lists a pressure-transducer system, as per their October 2026 specifications. Water still has to be measured against the mix, because extra water at the chute lowers the strength whatever the machine. Admixtures change early strength too; the concrete admixtures guide explains which do what.
Keep a cube register: cube number, date and time cast, grade, slump, where the batch went, and the 7-day and 28-day results beside each other. On a site with a quality engineer that register is part of the job, as the post on the QA QC engineer in construction describes. More concrete and material topics are in the building materials guides.
Pouring regularly and want batching you can trust? Compare concrete mixer models and prices and talk to a dealer near you.
The method and figures on this page are from IS 516 (Part 1/Section 1):2021, Hardened Concrete: Testing of Strength and IS 456:2000, Plain and Reinforced Concrete, Code of Practice, with cube making and curing from IS 1199 (Part 5):2018, core testing from IS 516 (Part 4):2018, ready-mix sampling from IS 4926:2003 and the mix design target from IS 10262:2019, all read in October 2026.
Prices, specifications and features are indicative, vary by variant, location and date, and should always be confirmed with the official OEM or authorised dealer before any purchase decision. DesiMachines is not liable for decisions taken on the basis of information that may have changed after publication. Code requirements on this page are as published in IS 456:2000 (with amendments), IS 516 (Part 1/Section 1):2021, IS 516 (Part 4):2018, IS 1199 (Part 5):2018 and IS 4926:2003, read in October 2026; acceptance of concrete on a structural job is decided by the project’s engineer under the contract specification.
Machines, tenders and news for this industry: Building Construction